

Introduction: Why one small choice can ripple through your shop
Ever wonder why two shops with similar budgets end up with wildly different product quality? I do — and I ask that question because the data keeps pointing at process choices, not just capital. According to recent shop-floor surveys, a surprising percentage of downtime traces back to tool handling and control mismatches, not raw horsepower. As someone who talks to vertical machining center manufacturers regularly, I see the pattern: decisions made at purchase time echo for years (and sometimes they cost more than the machine itself).
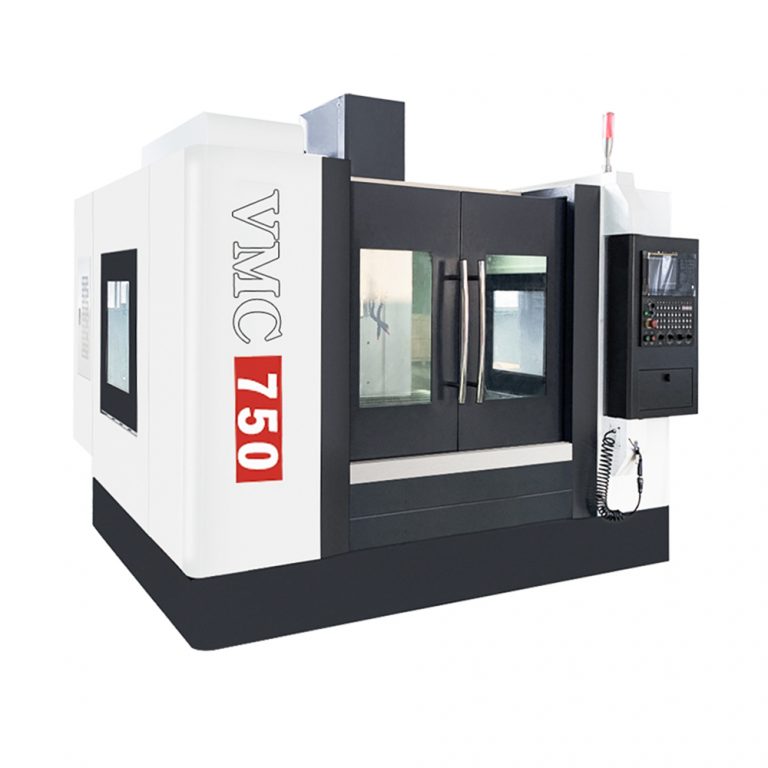
I want to be clear: I’m not lecturing. I’m sharing what I’ve seen firsthand — the small specs, like spindle speed options or the type of tool changer, that stack up into major production differences. When we weigh energy use, lifecycle maintenance, and cycle consistency, those specs matter. So where do most teams go wrong during selection — and how do you spot it before the first part comes off the table? Let’s drill into the hidden faults and practical fixes next.
Part 2 — The deeper flaw: why traditional fixes fail on the shop floor
When I look at a new line of work, the first thing I check is whether the proposal treats the machine as a black box. The truth is, many vendors still sell the idea that a “faster spindle” alone will solve throughput problems. But with a 5 axis vertical machining center, dynamics like tool change sequencing, coolant system design, and feedback from the CNC controller matter just as much. If you ignore interaction effects — for example, how the ATC (automatic tool changer) timing affects cycle time — you’re chasing a single metric that won’t deliver real gains. Look, it’s simpler than you think.
What’s the common snag?
Here’s the technical bottom line: legacy approaches optimize one axis at a time. They tune spindle speed or buy a higher torque servo motor without integrating controls, ball screw stiffness, or thermal drift compensation. That mismatch causes chatter, rejects, and surprise maintenance — so your mean time between failures drops. I’ve seen shops replace parts of a line to chase a few percent gain, only to find throughput unchanged because the coolant system or power converters weren’t tuned to the new load. These are engineering-level problems, but they start in procurement. — funny how that works, right?
Part 3 — What comes next: new principles that actually change outcomes
Going forward, I prefer to evaluate machines on systems, not specs. Modern work centers should behave like a network: the CNC controller, spindle drive, spindle motor, and even edge computing nodes must share performance data. For buyers who ask the right questions of a cnc vertical machining center supplier, the conversation shifts from “how powerful?” to “how coherent?” Coherent systems let you reduce cycle variance and predict maintenance windows. They also let you tune coolant flow and tool paths together so the part comes out right more often.
What’s Next
Practically, here are three evaluation metrics I use when I advise teams (and you can too): 1) Integration readiness — can the controller share live telemetry? 2) Thermal stability — does the spindle and ball screw design keep tolerances across shifts? 3) Lifecycle support — is spare parts logistics and software updates clear? These criteria help you see past marketing numbers and evaluate real shop-floor impact. I say this because I’ve watched small choices cost weeks of downtime; we can avoid that with smarter questions. In closing, keep your checklist focused on systems, not single specs — and if you want a reliable partner, consider talking to Leichman.
